Sejak tahun 2001, Shenheng Power telah menjadi produsen peralatan transmisi dan distribusi daya yang tepercaya, yang menghadirkan solusi kelistrikan yang andal secara global.
Didukung oleh sistem purna jual yang lengkap, kami menyediakan konsultasi teknis ahli, panduan produk, serta layanan OEM & ODM yang fleksibel untuk proyek Anda.
Sejak tahun 2001, Shenheng Power telah menjadi produsen peralatan transmisi dan distribusi daya yang tepercaya, yang menghadirkan solusi kelistrikan yang andal secara global.
A switchgear factory acceptance test (FAT) checks the manufactured equipment against the approved specification before shipment. It combines document review, construction inspection, applicable routine-test evidence and agreed functional demonstrations. A useful checklist identifies the exact panel, acceptance basis, witness responsibility and evidence required for each item. FAT does not prove that transport, site assembly, cable installation or final protection coordination will be satisfactory; those interfaces need their own site acceptance and commissioning checks.
This guide focuses on medium-voltage metal-enclosed switchgear. Adapt it to the actual technology, contract, standards and supplied configuration. It is a buyer’s inspection framework, not a generic instruction for applying high voltage to every device in a panel.
Agree the scope before the witness visit
The inspection and test plan should distinguish document review, hold points, witness points and records submitted for review. It should state what the buyer will observe and what the manufacturer completes independently. Agree the notice period, sample selection where permitted and the handling of a missed witness point.
Identify the equipment covered by each report. A project may contain incomers, feeders, metering panels, bus couplers and different breaker duties. A generic report bearing the project name does not establish that every supplied panel was inspected or tested as required.
The IEC 62271-200 catalogue scope addresses AC metal-enclosed switchgear above 1 kV up to and including 52 kV. The applicable edition and contractual amendments must be agreed. Its catalogue description identifies scope; the actual standard and specification determine the detailed requirements.
Separate type-test evidence from routine tests
Type-test evidence supports a design or defined configuration. Routine tests concern the manufactured equipment according to the applicable requirements. A witnessed FAT may include routine tests and additional contractual demonstrations, but it does not mean every design test is repeated on every panel.
Review whether supplied design evidence applies to the offered construction, ratings, components and arrangements. Record deviations for technical assessment. An internal-arc report for a different enclosure or accessibility arrangement cannot simply be treated as proof for every version carrying the same product family name.
The short-circuit rating guide helps distinguish the ratings that must align with the project study. The internal arc classification guide explains another important boundary: classification evidence and installation conditions must be checked against the actual offer.
Review the approved documents first
Collect the approved single-line diagram, general arrangement, panel schedule, wiring diagrams, component list, ratings and protection philosophy. The drawing revision on the factory floor should match the revision used by the inspector. Resolve changes before executing a functional demonstration against an obsolete scheme.
Check nameplates, panel identifiers and serial numbers. Confirm that the records can be traced from the report to the physical equipment and later to the installed location. If a report covers multiple panels, the identification list should be explicit.
Review manufacturer documentation for major components and any agreed design-test evidence. Record exceptions and exclusions. A missing document is an open acceptance item, even if the panel looks complete and the operating mechanism moves correctly.
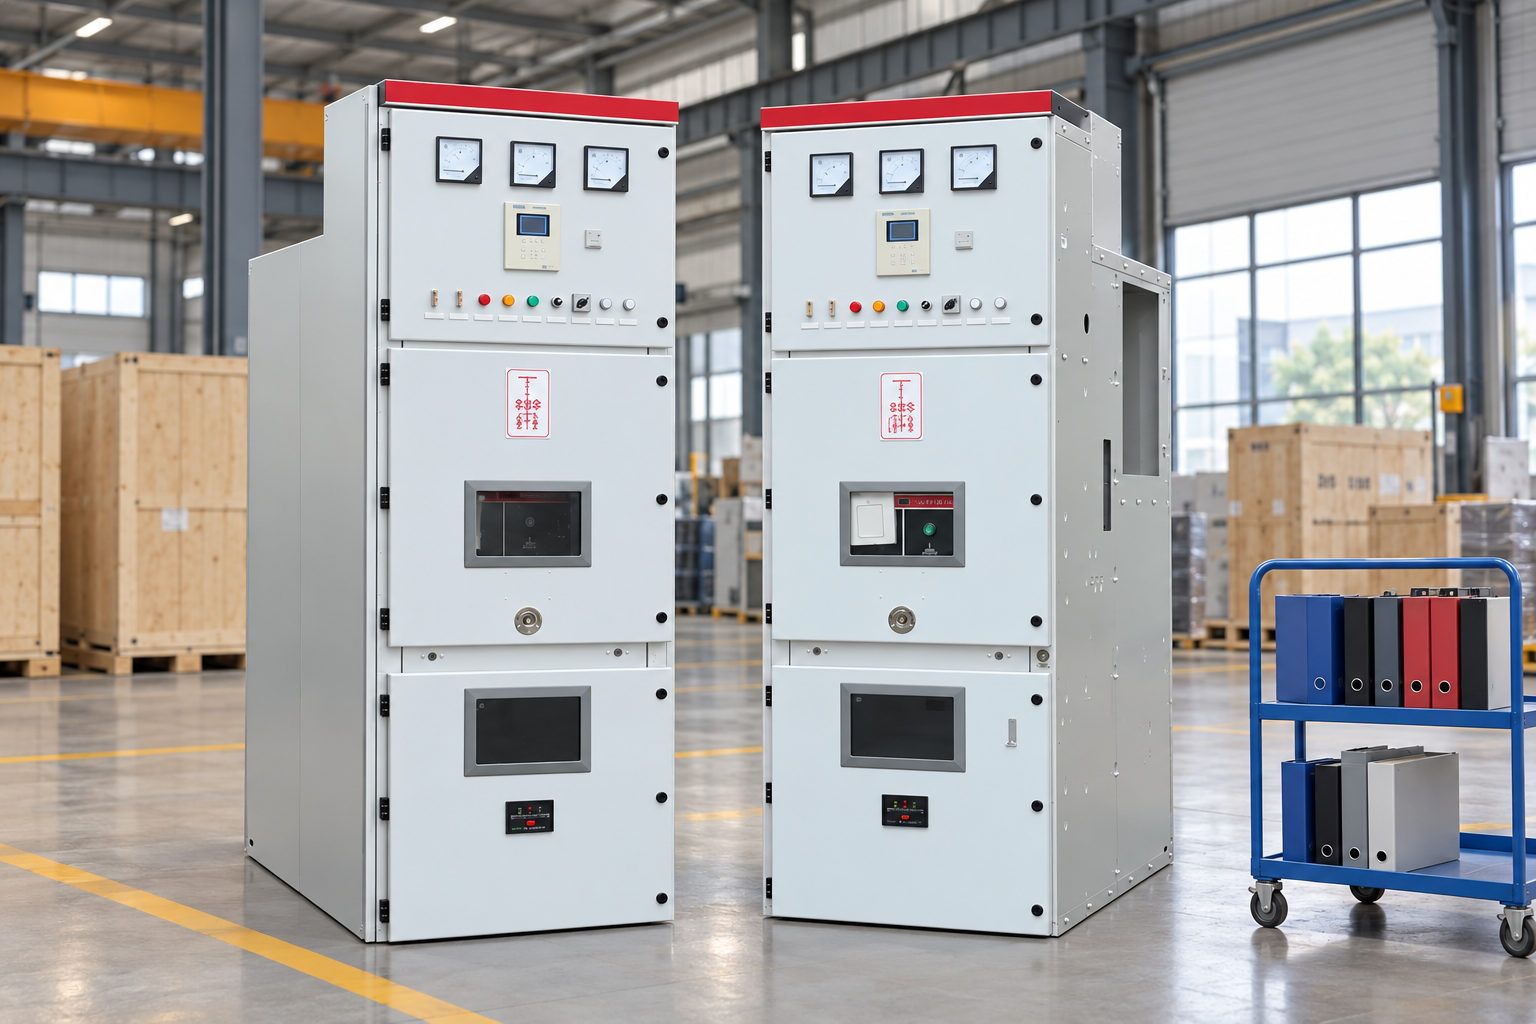
Record routine-test evidence and agreed functional demonstrations. Reference-based illustration.
Inspect the manufactured arrangement
Compare dimensions, panel sequence, accessible compartments, cable interfaces and transport sections with the approved arrangement. Confirm that the supplied configuration leaves the agreed installation and maintenance access. Do not infer the final site clearance from a cabinet standing alone in the factory.
Inspect visible workmanship, labels, enclosure condition and the documented earthing arrangement through the authorized inspection procedure. Confirm that the specified major components are present and identifiable. Any substitution needs the agreed approval process rather than a verbal explanation during the witness visit.
Check auxiliary supply ratings, control devices, terminal identification, heaters and monitoring options where included. These details can affect the site integration even when the main circuit ratings are correct. Record the actual delivered option, not a feature shown in a marketing photograph.
Use a panel-specific acceptance checklist
The table provides a starting structure. Detailed test parameters and limits must come from the agreed standard, manufacturer instructions and approved inspection plan.
FAT area
What to verify
Acceptance basis
Record to retain
Identity and drawings
Panel, serial number, function and revision match
Approved panel schedule and drawings
Signed identity list and revision register
Main ratings
Voltage, current and short-circuit duty align
Contract and approved study requirements
Nameplate record and technical schedule
Design evidence
Applicable reports cover the offered arrangement
Agreed standard and accepted deviations
Traceable report references and review outcome
Construction
Components, interfaces and workmanship match
Approved bill of materials and arrangement
Inspection checklist and deviation photographs
Routine electrical tests
Required tests cover the supplied equipment
Applicable routine-test procedure
Instrument output and panel-specific results
Mechanical operation
Permitted operating states function correctly
Equipment instructions and interlock matrix
Witnessed operation record
Perlindungan dan kontrol
Inputs, outputs, alarms and trip paths match
Approved logic and wiring diagrams
Functional test sheets and configuration version
Shipment release
Blocking items closed and documents complete
Contractual release criteria
Signed release or explicit hold record
Witness electrical tests through approved procedures
The test plan should state the measurement scope, equipment configuration, instruments, applicable limits and precautions for connected components. Insulation measurements, dielectric tests and circuit resistance checks answer different questions. They should not be grouped under an unexplained “electrical test passed” label.
Some components may need a specified treatment before a particular test. The manufacturer’s procedure establishes that configuration and its restoration. A checklist that applies one test voltage indiscriminately to every connected electronic device can damage equipment and does not demonstrate sound acceptance practice.
Instrument identification and calibration status should be recorded where required. Preserve raw results and any retest sequence. If a failure is corrected, retain the original result, corrective action and accepted retest so the buyer can understand what changed.
The IEC 62271-1 catalogue page provides common-specification context for high-voltage switchgear and controlgear. Confirm the edition and applicable product requirements rather than assuming one catalogue page supplies all test limits.
Test interlocks as a matrix of allowed and blocked states
Agree the intended operating states from the actual design. Test both permitted actions and prohibited operations using the manufacturer-approved method. A demonstration that only shows successful closing leaves important interlock functions unverified.
Record the equipment state, command, expected outcome, actual outcome and witness. Include the applicable local and remote controls, breaker position indications and earthing arrangements. The earthing switch interlock guide helps prepare these questions without replacing the panel’s actual logic matrix.
For withdrawable equipment, the approved procedure may include relevant service, test and disconnected positions. For fixed equipment, the applicable operating arrangement differs. The fixed versus withdrawable switchgear comparison explains why one generic demonstration sequence cannot cover every design.
Verify protection and control without overstating the outcome
Factory functional checks should verify the supplied wiring, specified devices, indications, alarms and agreed trip paths. Identify simulated interfaces and unavailable site equipment. A relay output demonstrated at the factory does not prove a remote installed breaker or final supervisory system will operate correctly at site.
Record relay model, firmware where relevant, configuration revision and the settings used for the demonstration. Distinguish temporary test settings from the final approved settings. A contractor should not copy the factory test file into service without the protection engineer’s approval.
The university video below explains relay testing and commissioning principles. It supports this protection-and-control section, rather than claiming to demonstrate the entire switchgear FAT.
Further learning: Lecture 39 Testing, Commissioning and Maintenance of Relays-I — IIT Roorkee July 2018. This educational video supports the topic; it is not a product demonstration or an operating authorization. Buka video di YouTube.
Close shipment-blocking items and preserve the as-built records. Reference-based illustration.
Manage deviations and release decisions
Use an itemized list with the panel, requirement, observed deviation, proposed action, owner and closure evidence. Classify which items block shipment and who has authority to accept a concession. A signature on a witness sheet should not quietly become unconditional acceptance of every open issue.
After corrective work, decide which checks need repetition. Replacing a component or altering wiring can affect an earlier accepted result. The retest scope should follow the change, and the final document package should show the as-built arrangement rather than the original plan.
Photographs help identify the issue but do not replace measurements or signed records. Store them with the relevant item reference. A folder of unlabeled cabinet photographs is difficult to use once the equipment has been split into transport sections.
Prepare shipment and site handover
Confirm packing, transport restraints, environmental protection, accessory inventory and installation instructions. Record any equipment removed or secured for transport and how it is to be restored. Include lifting and handling documentation appropriate to the supplied arrangement.
The handover package should contain final drawings, routine-test records, applicable design evidence, component manuals, relay configuration details and the closed deviation list. Retain an explicit record of unfinished interfaces that require site verification. The NETA acceptance testing standards page provides context for an applicable field acceptance framework; it does not turn the factory witness visit into site commissioning.
When discussing the KYN28 switchgear offer, request the actual configuration and proposed inspection plan. Confirm the insulation system and test evidence in the offer. Product naming or a photograph cannot establish compliance, internal-arc classification or the scope of completed tests.
Before shipment release, reconcile every transport section with the final panel list and document package. Confirm that the buyer knows which records accompany the shipment and which are delivered separately. If a contractual concession remains open, include its limitations and agreed closure point in the handover. This prevents the site team from interpreting a factory release as evidence that an unresolved interface has already been accepted. The release record should make the remaining work visible and assign it to the responsible party.
Pertanyaan yang sering diajukan
Is FAT the same as a type test?
No. FAT is an agreed factory acceptance process. It can include review of applicable design-test evidence, routine tests on the supplied equipment and contractual functional demonstrations. Its exact scope must be defined in the inspection plan.
Does a completed FAT remove the need for site acceptance?
No. Transport, assembly, installed cables, earthing, final protection settings and external interfaces require site-specific verification. Factory records provide evidence and a baseline, but do not prove the final installation.
Should every test be repeated after a factory correction?
The responsible engineer should define the retest scope from the change and its effects. Retain the original finding, corrective action and relevant retest evidence instead of replacing the history with an unexplained pass.
What should prevent shipment release?
The contract and approved inspection plan define blocking conditions. Unresolved safety, functional, rating or documentation issues should be assessed by the authorized acceptance team and explicitly closed or formally dispositioned before release.
Shenheng Electric Power berkomitmen untuk menjadi pemimpin global dalam solusi peralatan listrik, membantu pelanggan mencapai manajemen daya yang aman, efisien, dan berkelanjutan.
 PT Shenheng Power Equipment Co., Ltd.